An engineering office
with a workshop attached.
Most equipment suppliers are workshops that buy drawings. We are the other way round: a process engineering team that owns the fabrication floor, which is why a drawing revision reaches the steel in days rather than months.
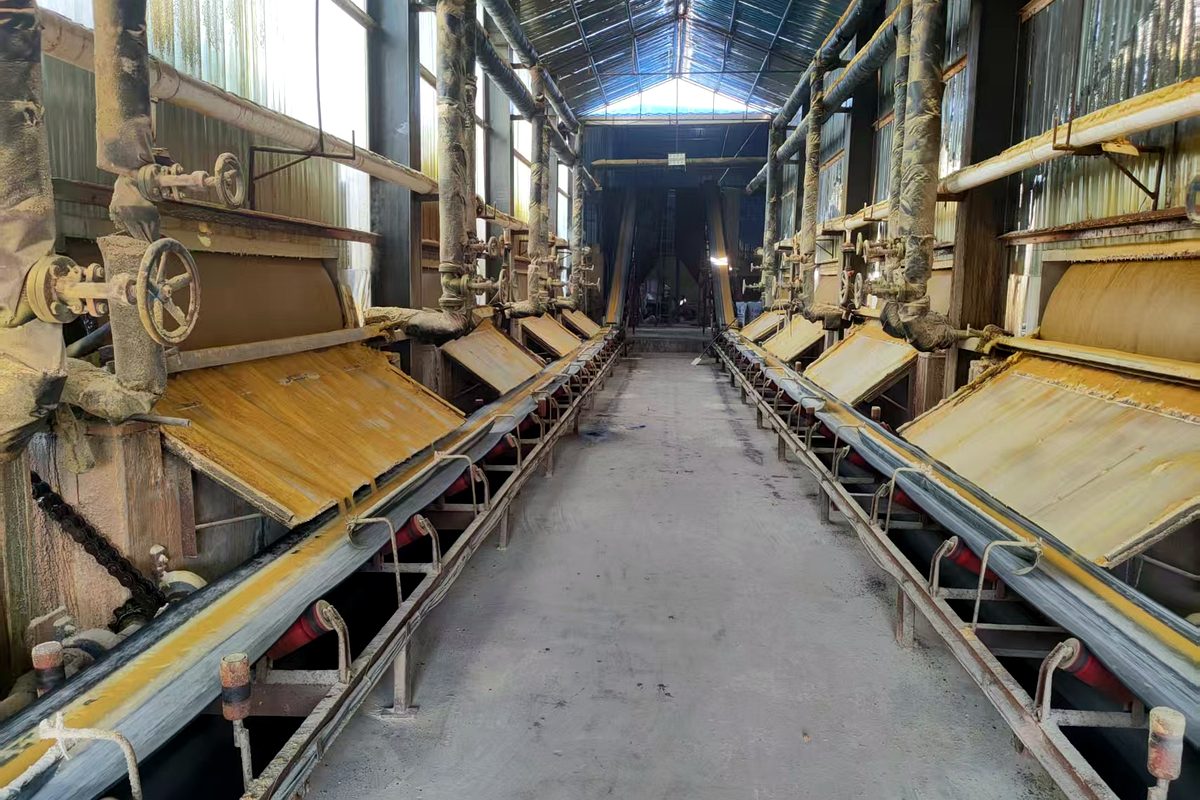
Design-led, not catalogue-led.
The distinction sounds academic until something goes wrong on site.
GARUN started in 1992 building equipment for coagulant plants in Henan. Over three decades the work moved upstream: clients kept asking why a plant did not perform, and the answer was almost never the steel — it was the layout, the sizing, the utilities, the absence of a mass balance. So we built the engineering capability first and kept the workshop behind it.
Today a project runs from a design basis written with the client, through a 180–260 sheet drawing set, into our own fabrication hall, and out to a site where the same engineers supervise erection and commissioning. One team, one set of drawings, one party to call.
8,000 m², forty minutes from the airport.
Vessels, drums, towers and ducting are all built and trial-assembled under one roof before they are packed.
- Plate rolling up to 30 mm, with automatic welding on longitudinal and circumferential seams
- Lining bay for rubber, vinyl-ester FRP and acid-resistant tile, with spark testing on site
- Assembly floor with overhead crane capacity for 50 m³ vessels and 2 m drums
- Drum machining and dynamic balancing for dryer shells and agitator shafts
- Trial assembly of towers, ducting and platforms before shipment, photographed for the client's records
- Packing bay with frame packing, flange protection and desiccant for electrical enclosures
Documented, per equipment tag.
Certificates are not a marketing claim; they are a set of records that travel with each item.
| Record | Scope | Issued |
|---|---|---|
| Material certificate | Plate, pipe, forgings — mill certificate with heat number | Per item |
| Weld record | Welder ID, procedure, seam map, NDT result where required | Per vessel |
| Lining test | Spark (holiday) test at 5 kV, thickness readings, cure record | Per lined item |
| Pressure test | Hydrostatic at 1.5× design where the item is a pressure part | Per vessel |
| Dimensional check | Nozzle orientation, overall dimensions against the GA | Per item |
| Trial assembly | Photographic record of assembly before packing | Per system |
| Third-party inspection | SGS or CCIC witness and certificate, on request | Per shipment |
The dossier is issued in English with the equipment. Nothing is held back pending final payment.
Design work follows the same discipline: each discipline checks the other's drawings before release, calculations are filed against the drawing they support, and every sheet carries a revision status. It is unglamorous and it is the reason a plant can be built from our drawings by a contractor who has never met us.
China, and wherever the plant goes.
Design and fabrication in Zhengzhou; erection and commissioning on the client's site.
Export packing, English documentation and shipping to the client's port are routine. For overseas projects we normally send a commissioning engineer for erection supervision and the trial run, and support the plant remotely afterwards with a named contact.
We are deliberately conservative about what we claim. This site states capacities, tolerances and programme durations as ranges because that is how they behave in practice. Where a figure depends on your raw material or your site, we say so and calculate it with you rather than quote a number that flatters the brochure.